

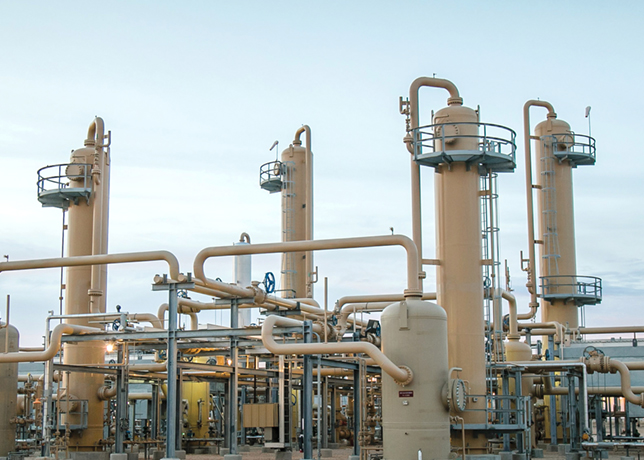

Sulphur recovery units (SRUs) play a critical role in modern gas processing and refining facilities, and while sulphur production is the ultimate objective, reliable handling of numerous auxiliary process fluids is equally important for safe and efficient operation.
Within Claus units, canned motor pumps are frequently used for sour water, wash water, reflux, condensate and other critical duties where containment and reliability are essential.
Many SRU fluids contain dissolved hydrogen sulphide (H2S), corrosive compounds, hydrocarbons or contaminated water.
Continuous operation and strict environmental requirements make process containment a key design criterion.
The hermetically sealed design eliminates mechanical seals and, therefore, removes the principal dynamic leakage path found in conventional centrifugal pumps.
This supports improved safety, lower emissions and reduced maintenance.
Modern canned motor pumps can be supplied in accordance with API 685 for sealless centrifugal pumps and are commonly designed around ISO 15783 requirements.
Hydraulic designs can also be based on ISO 2858 dimensions where applicable, facilitating integration into industrial process plants.
A key component of Hermetic canned motor pumps is the hydrodynamic slide bearing system operating in the pumped liquid.
During normal operation, there is no metal-to-metal contact.
Hermetic commonly utilises a proven bearing combination consisting of tungsten carbide coated bearing sleeves (W5) and silicon carbide bearing bushings (SiC30).
This combination provides excellent wear resistance, chemical resistance, thermal shock resistance and long service life, while remaining essentially maintenance-free under normal operating conditions.
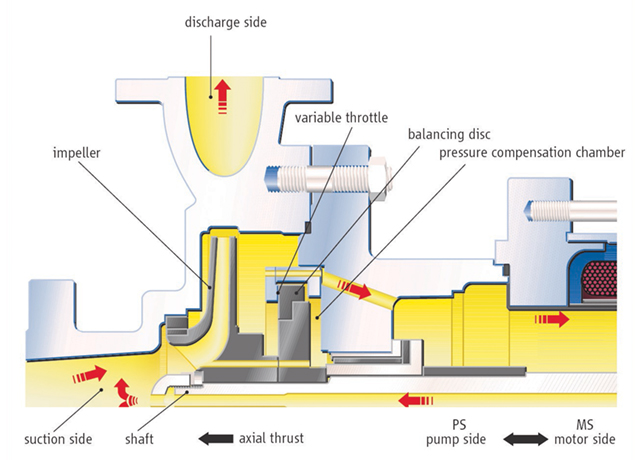
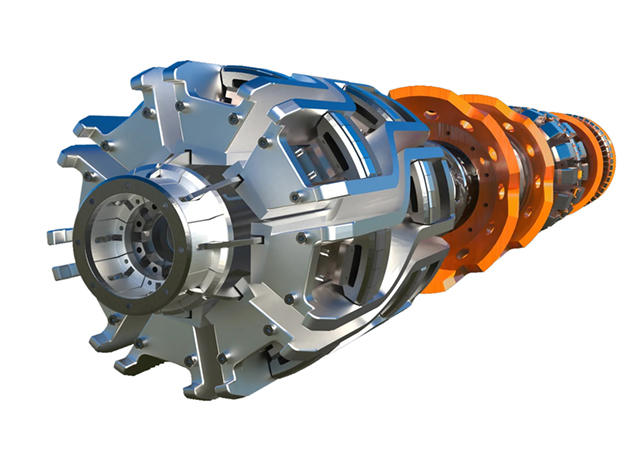
A diagram of the advanced axial thrust balancing system in a canned motor pump
ADVANCED AXIAL THRUST BALANCING TECHNOLOGY
One of the key engineering challenges in canned motor pump design is the management of axial thrust forces acting on the rotor assembly.
Unlike conventional pump arrangements that may rely on dedicated thrust bearings, Hermetic canned motor pumps utilise a hydraulic balancing concept specifically developed to continuously compensate axial forces during operation.
The Hermetic balancing system is based on a variable throttling arrangement integrated into the balancing disc.
As the rotor position changes, the pressure inside the compensation chamber automatically adjusts, creating a self-regulating hydraulic balancing effect.
This design offers several advantages:
• Continuous automatic axial thrust compensation.
• Reduced load on bearing components.
• Improved rotor stability.
• Minimised wear during operation.
• Extended equipment lifetime.
• Enhanced reliability in continuous process applications.
By maintaining a balanced operating condition throughout the pump’s operating range, the system contributes significantly to the long service life and operational reliability expected in demanding refinery, petrochemical and gas processing environments.
Typical applications include sour water pumps, wash water circulation pumps, reflux pumps, condensate transfer pumps and other auxiliary services where fugitive emissions and maintenance must be eliminated.
In large gas processing and refining facilities across the Middle East and worldwide, operators continue to rely on sealless technology to support long-term operational performance, process safety and environmental objectives.
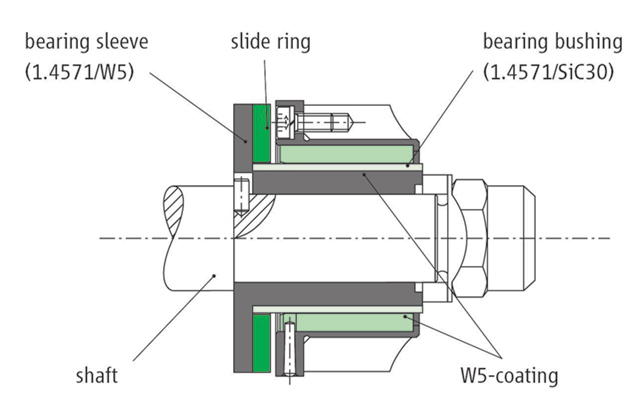
A cross-section of the hydrodynamic slide bearing system
BEYOND AUXILIARY SERVICES: MOLTEN SULPHUR TRANSFER
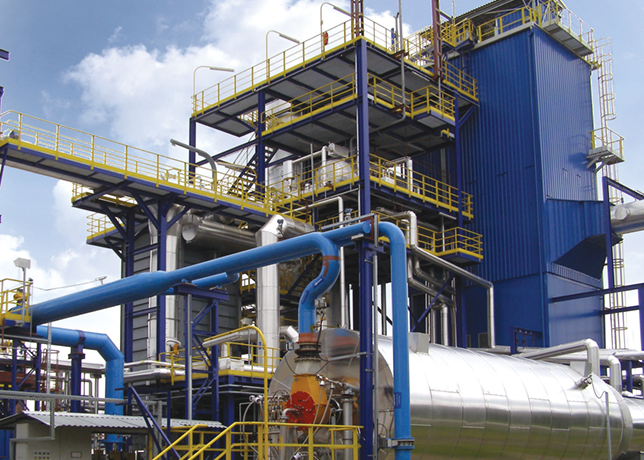
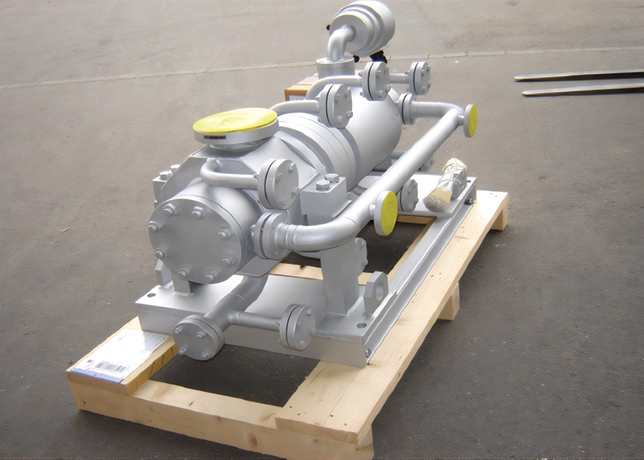
In addition to Claus process services, canned motor pumps can also be engineered for molten sulphur applications.
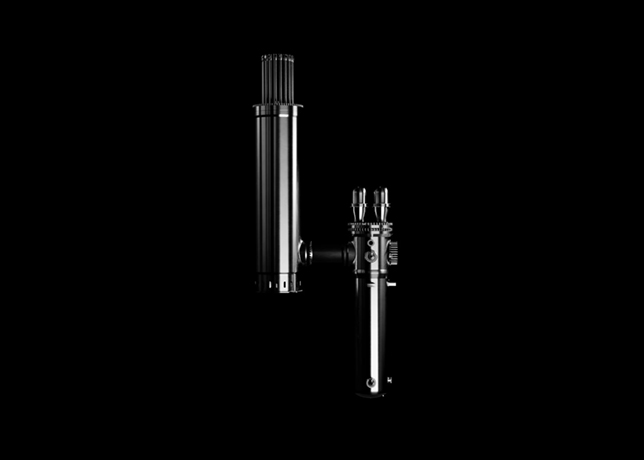
These designs incorporate dedicated thermal management and heating arrangements to prevent sulphur solidification and ensure reliable operation in one of the most demanding services within a sulphur recovery plant (Figure 1).
Specially engineered Hermetic canned motor pump for molten sulphur service.
Hermetic-Pumpen is a leading developer and manufacturer of hermetically sealed pumping technologies.
Recognised worldwide for its expertise in canned motor pump technology, HERMETIC has built a strong reputation for providing safe, reliable and long-lasting solutions for demanding industrial applications involving hazardous, toxic, corrosive and environmentally sensitive fluids.
Hermetic pumps are designed to operate under some of the most challenging process conditions encountered in the oil and gas, petrochemical, chemical and energy industries, covering fluid temperatures from -160 deg C up to +480 deg C and system pressures up to 120 MPa.
With power ratings ranging from 1 kW to 690 kW, Hermetic offers one of the broadest canned motor pump portfolios available on the market, including solutions for refinery processes, gas processing facilities, sulphur recovery units, LNG applications and other critical services requiring maximum process containment.
Headquartered in Germany, Hermetic employs approximately 400 people and maintains subsidiaries in China and the US.
Together with its global network of service centres and authorised partners, the company provides comprehensive support throughout the entire lifecycle of industrial installations, from project engineering and commissioning to maintenance and aftermarket services.
HERMETIC-Pumpen is exhibiting at Stand 8718, Hall 8.